How to Start an AAC Block Business: Plant Setup Guide
2026-09-28
View:9
Starting an AAC block business is a capital project before it is a manufacturing one. This guide is for the investor or building-materials manufacturer who already has capital and a market, and now needs the actual sequence: how to start an AAC block business without overbuilding capacity the local market cannot absorb, and without underbuilding it and losing the payback case.
The outcome is a commissioned plant with a capacity matched to local demand and a payback you can defend to a lender. Getting there means working through six decisions in order, from demand validation and the capex envelope through site and raw-material supply, production line configuration, licensing and financing, to commissioning and ramp-up. Each step opens with the criterion you are judging against, then the action.
This guide is published by Teeyer, a company founded in 1989 that has specialized in the AAC industry for over 35 years and has built more than 1,200 AAC production lines globally across 30 countries. Its work covers turnkey project management from investment analysis to operation, raw material analysis and formulation, equipment installation and service support, and production management consulting. That direct involvement in planning and commissioning AAC plants is the basis for the guidance in this article.
How to Start an AAC Block Business: The Six Decisions That Decide the Project
Starting an AAC block business is a sequence problem before it is a construction problem. Six decisions determine whether the plant ever reaches its designed output, and they have to be made in order: demand absorption, capacity and capex, site and raw materials, equipment and line configuration, licensing and financing, then commissioning and ramp-up.
The order matters because nameplate figures and saleable output diverge. Nameplate design, whether 100,000, 200,000 or 300,000 m³ per year, and actual saleable production are rarely the same number. The gap traces back to seven bottlenecks that keep an AAC plant below designed capacity, from raw-material preparation through autoclave scheduling.
The pattern is not new. AAC Worldwide reports that over 70% of China's 3,000-plus AAC factories are more than a decade old, averaging below 60% capacity utilization, with low capacity utilization from slow production cycles and poor mould turnover among the named failure modes.
Key Takeaway:AAC block production line capacity is chosen by demand absorption, not by what a vendor can quote.
Step 1: Validate Local Demand Before You Size Anything
Before you price a single machine, establish how many cubic metres of AAC your delivery radius can absorb each year. That number, not the equipment catalogue, sets everything downstream.
These are market-level figures. They do not prove your region will absorb your output, and treating them as proof is the most common way new plants get sized wrong.
Build the estimate yourself: count the permitted new-build pipeline inside your economical delivery radius, subtract competing supply including imported and neighbouring-region blocks, and confirm which specification the local market actually buys. EN 771-4, ASTM C1693 and IS 2185 are the markers that tell you what "compliant block" means in your market, and a plant built to the wrong one sells nothing.
Verification checkpoint: you should now hold a written demand estimate in m³/year, with the sources and assumptions behind it. This is the first input to your AAC block manufacturing business plan.
Step 2: Match Plant Capacity to Demand and Set the Capex Envelope
By the end of this step you should hold two numbers: a capacity band in m³ per year, and a capex envelope whose scope you can compare, line by line, against a real quotation.
The capacity band is your first anchor. Core line equipment covers batching, mixing and pouring, the cutter, autoclaves and handling, and it moves with region, capacity and automation level. The larger the annual output band, the more the core machinery package grows, so treat any single quoted range as a starting point for comparison rather than a fixed price.
Equipment is not the whole bill. Scope matters more than the headline: a realistic investment figure includes machinery, autoclaves, utilities, site works, installation, initial raw-material stock, licences and contingency, and excludes working capital, land acquisition and financing costs. If your quotation does not draw the same line, you are comparing two different projects.
Automation is a decision, not a default. Full automation raises plant capex and cuts labour from 50 workers to 15. Run the labour saving against your local wage bill before accepting it.
Capex breakdown for a 200,000 m³/yr AAC block plant, low and high case
Line item
Share of total
Land and civil works
15-20%
Machinery and equipment
50-60%
Installation and commissioning
5-8%
Initial raw-material stock
5%
Utilities and boiler
10%
Licences and contingency
5%
Total
100%
One specification choice sits inside that machinery line: fixed cutter systems cost more but deliver 99% dimensional accuracy, the difference between selling to specification and sorting rejects.
Verification checkpoint: your capex envelope is ready when every line item has a stated scope and a low/high range, so a vendor quotation maps onto it line by line rather than being accepted as one lump sum.
Step 3: Secure the Site, Utilities and Raw-Material Supply
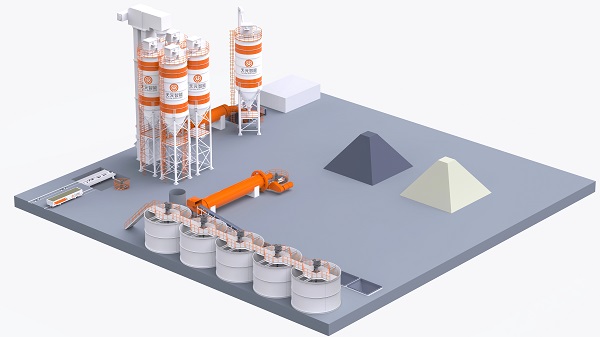
Land, power, water and raw materials are the preconditions that decide whether a plant ever reaches its designed output. A standard 200,000 m³/yr AAC plant needs roughly 8 to 12 hectares and 120 to 160 workers, according to a Market Reports World AAC market summary. Size the yard for stockpiles, the autoclave hall, curing and finished-goods storage before you commit to a layout.
Raw-material sourcing deserves more scrutiny than most guides give it. Fly ash from different sources varies in fineness and unburned carbon, sand shifts with seasonal moisture or clay contamination, and lime reactivity shifts between batches. These are structural variables, not occasional defects.
The right selection criterion is cost per usable ton of product rather than price per ton of raw material, because unstable inputs translate into breakage, line stops and lost shifts. Note too that siliceous materials, including fly ash, often require crushing and grinding before use, so the grinding circuit is a process requirement rather than a sand-only cost.
Verification checkpoint: you should hold a tested formulation derived from your own locally available materials, not a supplier's generic recipe.
Step 4: Choose the Production Line Configuration and Equipment Scope
A line specification is only as good as its weakest section, and the seven bottlenecks that keep an AAC plant below designed capacity are usually found in raw-material preparation that cannot feed the line consistently, pre-curing treated as a hidden waiting zone, cutting capacity that fails once the full cycle is counted, autoclave scheduling that restricts the whole factory, and unreliable material handling, mould turnover or utilities.
Walk the five sections and name the control variable that decides output at each. Raw-material processing sets slurry density and temperature. Batching and pre-curing sets rising height, because dosing determines raw-material proportion, slurry fluidity and viscosity. Cutting sets tolerance. Autoclaving sets the pressure and temperature cycle, where differences in cake temperature and excessive water contribute to sticking and unwanted fusion. Finishing and packing sets first-pass yield. If material ratio, water content, temperature and aluminium addition are not controlled, later stages absorb the damage.
A turnkey EPC route is one way to hold that scope under a single supplier. Teeyer supplies turnkey AAC block and panel lines up to 1,000,000 m³ per single line, with DCS on Siemens PLC hardware, MES monitoring and ERP integration. The knowledge base carries no quantified customer case outcomes, so treat vendor capacity claims as specifications to verify, not results.
Verification checkpoint: your line specification names each section's throughput and the bottleneck you expect to bind first.
Step 5: Clear Licensing, Environmental Compliance and Financing in Parallel
Permits and money run on the same clock, and the slower one sets your commissioning date. Treat them as a parallel track rather than a sequence you start after equipment selection.
Four approval categories need checking with your own authority, because the requirements differ by jurisdiction: industrial land use and zoning, environmental approval covering dust, boiler emissions and wastewater, building-product certification to the standard your market enforces, and business registration. Regional permitting law, local tax treatment and specific lender terms sit outside what this guide can credibly state. Confirm them with your local planning, environmental and tax authorities, and with the lender directly.
On financing, the Step 2 capex envelope defines your debt and equity split. Build the payback figure from your own utilization and price assumptions. A vendor best case will quote you a short payback on a 200,000 m3/yr plant, but such a figure typically states no utilization rate, no discount rate and no ramp-up period, and it sits against ageing plants averaging below 60% capacity utilization. Cost per usable ton of product, not cost per ton produced, is what your model has to survive.
Warning: Model at 70% utilization first, and treat any payback under 24 months as a best case requiring justification.
Verification checkpoint: you are ready to approach lenders when you hold a permit checklist with a named owner and lead time for each item, and a payback model that still clears your debt service at 70% utilization.
Step 6: Commission, Certify Operators and Ramp Up to Designed Capacity
Commissioning proves the line, not the feasibility model. Run the sequence in order: dry-run each machine, then the batching and pre-curing section, then cutting, then the first autoclave cycles under manual supervision before handing control to the DCS. Certify operators on the same schedule, because the ramp-up gap usually traces to autoclave cycle time, batching accuracy, curing control and operator skill rather than to equipment.
Expect to miss nameplate capacity for the first 6 to 12 months. Producing 800 m3 a day means little if 5-8% needs rework, downgrade or disposal. Ageing plants show the same failure modes in slower form: steam consumption exceeding 200 kg/m3, slow production cycles and poor mould turnover, with roughly 20% thermal loss (aac-worldwide, 2023).
Modernised lines set the benchmark. New factories with automated lines achieve daily output exceeding 3,000 m3 and steam consumption below 100 kg/m3, and one retrofit cut steam from 200 to 100 kg/m3 (aac-worldwide, 2023). The same source reports that post-retrofit per-capita productivity rose from 4,000 m3/year to 12,500 m3/year, with average efficiency improvement of 35% and payback under two years.
Verification checkpoint: track measured first-pass yield and steam consumption per m3 weekly against the design figures. If steam sits above 120 kg/m3 or rework exceeds 5% after month three, the constraint is in the cycle or the cure, not in the market.
Common Mistakes That Keep New AAC Plants Below Capacity
Most underperforming AAC plants were sized on a vendor quote rather than on demand absorption, and the gap only shows up after commissioning. Audit your own feasibility model against the failure modes below before you commit capital.
Sizing from nameplate instead of saleable output. Nameplate design and actual saleable production are rarely the same number, and the difference compounds across every downstream assumption in an AAC block plant payback period calculation.
Treating raw-material variability as incidental. Fly ash from different sources varies in fineness and unburned carbon, so formulation is a structural input, not a one-time setup task.
Counting cutting capacity from the machine spec. The machine rating ignores the full cycle, including pre-curing, and the seven bottlenecks that keep an AAC plant below designed capacity sit across sections, not inside one machine.
Letting pre-curing become an unmanaged waiting zone. Uncontrolled dwell time feeds directly into the 5-8% of output that requires rework, downgrade or disposal.
Modelling payback at full utilization. Average capacity utilization below 60% is common, and cost per usable ton, not cost per ton produced, is the figure that survives contact with operations.
Warning: The single highest-cost mistake is a feasibility model built on nameplate capacity rather than saleable output. Every capex, margin and payback figure downstream inherits that error.
Frequently Asked Questions
What is the realistic minimum capital for AAC block plant setup cost?
The smallest practical entry point is a 30,000-200,000 m³/yr line, where the core line equipment package is at its lowest. That covers production machinery only. Add land, buildings, autoclaves, boilers, installation and working capital, and the total realistic investment rises well above the machine quote. Budget from the total scope, not the machine quote.
How long does it take from decision to first saleable block?
Plan on 12 to 18 months for a greenfield plant. Site preparation, permitting and equipment fabrication consume most of that window, with autoclave and boiler installation on the critical path. Commissioning and curing trials add several weeks before the first block meets density and strength targets.
Can a sand-based line be converted to fly ash, or the reverse?
Conversion is possible but not symmetrical. Siliceous materials often require crushing and grinding before use, so a fly-ash line moving to sand needs a grinding circuit added at the front end, a significant capital and layout change. Moving from sand to fly ash is generally simpler, though you must confirm consistent fly-ash chemistry and supply first.
What capacity utilization will a lender underwrite?
Lenders typically stress-test against average capacity utilization below 60%, even when the business plan projects higher. The gap is deliberate: it protects debt service if demand ramps slower than forecast. If your model only works above 70% utilization, expect the lender to decline or require more equity. Build your AAC block plant payback period calculation on the conservative case.
How much land and labour does a given capacity need?
As a rough planning guide, a 100,000 m³/yr plant needs roughly 10,000-20,000 m² of land including raw-material storage and curing areas, and 30-50 workers across three shifts. Smaller lines scale down proportionally, though the autoclave and boiler sections have a fixed footprint regardless of capacity. These are search-result planning estimates rather than measured benchmarks, so verify them against a specific equipment layout before committing to a site.
Conclusion
The six decisions above are the whole project in sequence: validate local demand before you size anything, match plant capacity to demand and set the capex envelope, secure the site and utilities and raw-material supply, choose the production line configuration and equipment scope, clear licensing and environmental compliance and financing in parallel, then commission and certify operators and ramp up to designed capacity.
Work them in that order and the outcome is concrete: a commissioned plant whose capacity was matched to measured local demand, with a payback modelled at realistic utilization rather than nameplate output. The capacity you size in Step 2 is the number every later cost and revenue line depends on, so it is worth getting right before committing capital.
If you would like help pressure-testing those numbers, Teeyer offers a feasibility and plant-configuration consultation: a review of your demand data, proposed capacity and site conditions, with a configuration recommendation and an indicative equipment scope. It is a consultation offer, not a substitute for your own due diligence, and you can request it through the Teeyer site.
```html
Pressure-Test Your Plant Numbers Before You Commit Capital
Send us your demand data, proposed capacity and site conditions. Teeyer reviews the feasibility, recommends a configuration and returns an indicative equipment scope, so your payback case holds up when it reaches a lender.